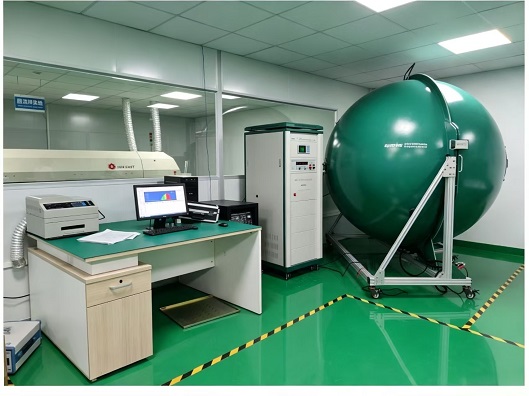
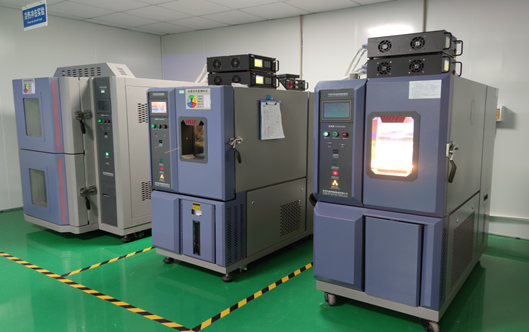
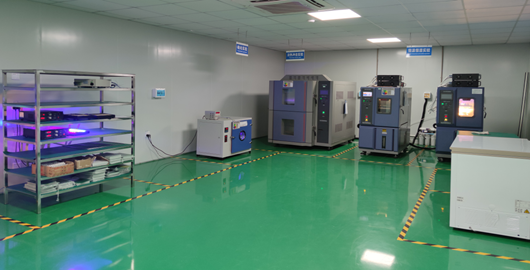
The Company has a professional R&D and testing laboratory, which is equipped with international benchmarking equipment, such as integrating sphere spectrometers, junction temperature optical thermal resistance testers, optical simulators, high and low temperature and humidity test chambers, and thermal shock test chambers, possessing comprehensive capabilities in analysis of photoelectric parameters and environmental reliability.
The laboratory has established a complete R&D closed loop from sample verification to introduction of mass production, focusing on three major directions: optical performance optimization, packaging process innovation, and failure mechanism analysis. Through a data-driven precise R&D model, it continuously drives improvements in luminous efficacy, reliability, and cost optimization of products, providing strong support for the Company's technological leadership and market competitiveness.